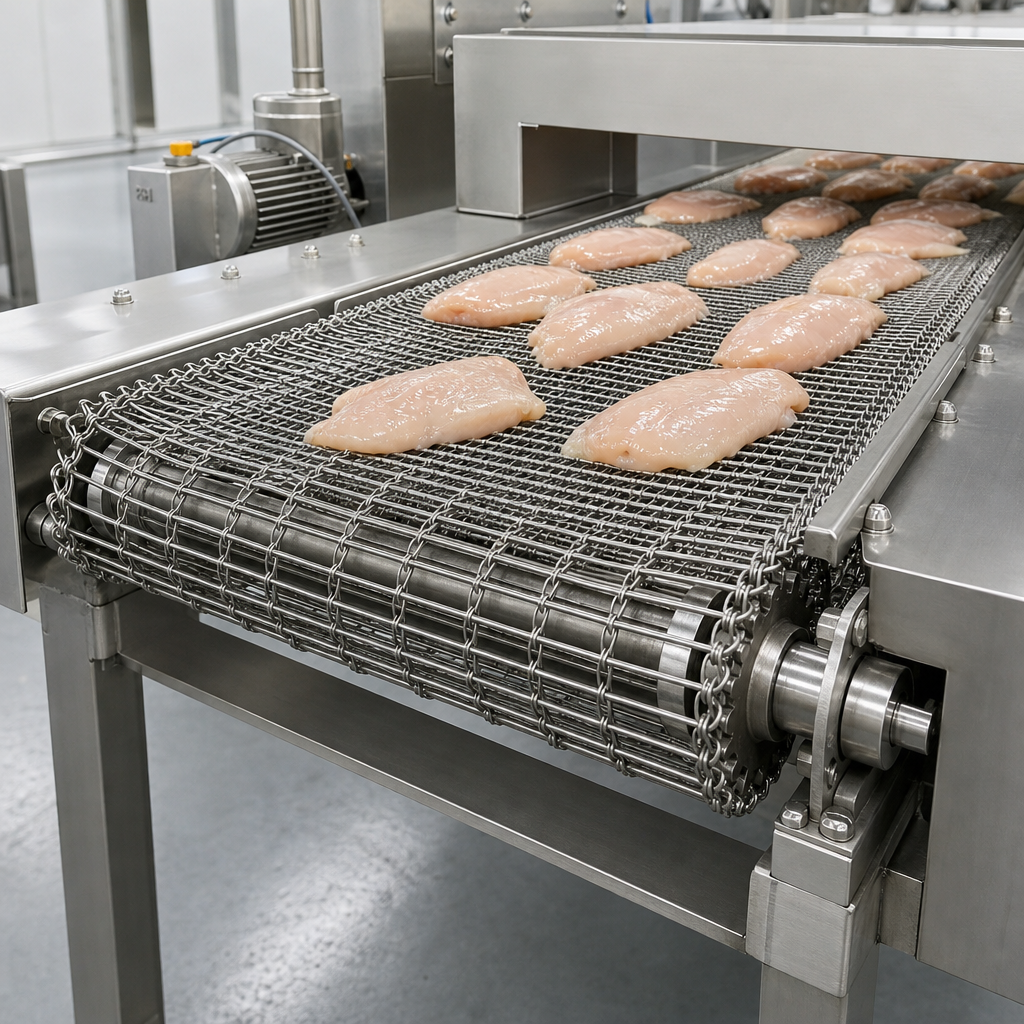
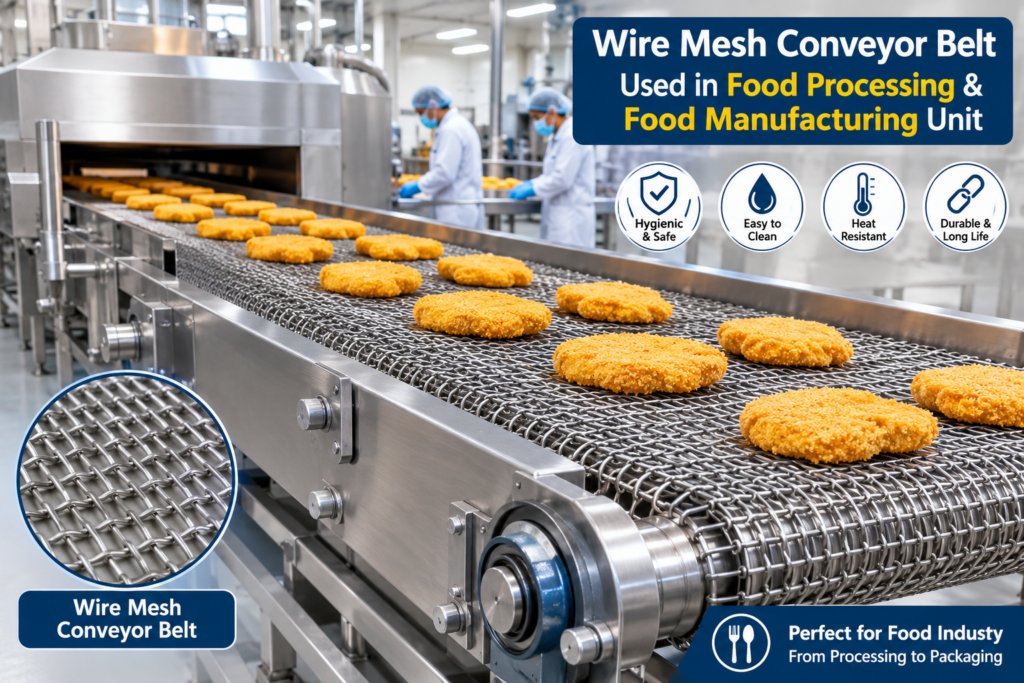
In modern food production, conveyor equipment does far more than transport goods from one station to the next. It must endure oven heat, blast-freeze cold, constant moisture, corrosive salts, and aggressive sanitation chemicals—all while helping facilities meet strict food safety standards. Wire mesh conveyor belts have earned their place as a core component in this environment because they combine open airflow, easy cleanability, and long-term durability in a way that solid belts simply cannot match.
Whether you are engineering a new line or upgrading existing infrastructure, it helps to understand how these belts perform across specific food sectors.